

Pneumatic conveying solution for grain pellets
During the processing, storage, and transportation of grain pellets, traditional mechanical conveying methods often face issues such as rapid equipment wear, severe dust pollution, high maintenance costs, and limited conveying distance. Especially for granular materials such as wheat, corn, rice, and soybeans, high crushing rates and frequent pipe blockages can affect production efficiency. At the same time, environmental compliance pressure is increasing, making enterprises urgently need cleaner, more efficient, and flexible conveying solutions.
Material characteristics
Grain particles are characterized by low density, uneven particle size, easy breakage, and large fluctuations in moisture content. For example, wheat has a bulk density of about 750~800 kg/m³, corn about 700~750 kg/m³, and rice husks are light and prone to dust generation. During conveying, it is necessary to avoid breakage caused by high-speed collisions and to adapt to seasonal humidity changes to prevent material adhesion or mold.
Product Introduction
The grain pneumatic conveying system provided by Head Powder uses positive or negative pressure pneumatic conveying technology, utilizing airflow through sealed pipelines to achieve long-distance, multi-branch material transportation. The system consists of a feeder, pipeline, separator, dust collector, and automatic control unit. It can be customized according to customer site layout, production requirements, and material characteristics to meet the full-process conveying needs from the granary to the processing workshop and from the dock to the silo itself.
Product advantages
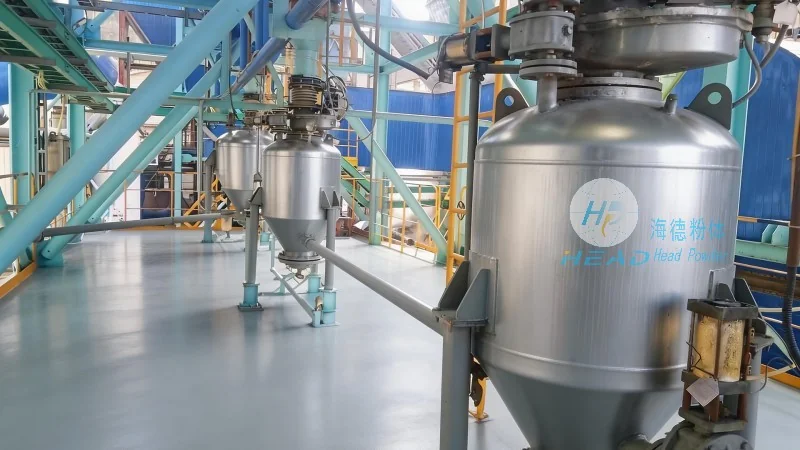
To address the pain points of traditional transportation, Head Powder's solution features the following features: fully enclosed system operation, no dust leakage, and compliance with environmental protection requirements; The conveying speed is adjustable, with a material crushing rate below 0.5%; Modular design supports flexible expansion and easy maintenance; The automatic control system monitors pressure and flow in real time, enabling intelligent anti-congestion and remote operation and maintenance, reducing the risk of manual intervention and downtime.
Product features

- Low Damage Conveying: By optimizing airflow speed and pipeline elbow design, the crushing rate of grain particles is kept at an extremely low level, protecting material quality.
- Fully enclosed and environmentally friendly: The system has no dust leakage throughout the process, requiring no additional dust removal equipment, meeting hygiene standards and environmental regulations in the food industry.
- Intelligent control: Equipped with PLC and sensors to automatically adjust conveying parameters, supports fault warning and remote control, reducing manual on-duty costs.
- Flexible customization: Based on conveying distance, height, output, and site space, we offer positive pressure, negative pressure, or combined solutions, compatible with various grain particles.
Product specifications

- Conveying capacity: 10~100 t/h (customizable according to customer requirements)
- Conveying distance: horizontal ≤500 m, vertical ≤ 50 m (single machine)
- Working pressure: Positive pressure 0.05~0.5 MPa / Negative pressure -0.05~-0.08 MPa
- Applicable materials: granular grains such as wheat, corn, rice, soybeans, sorghum, etc