

Pneumatic conveying scheme for pharmaceutical excipients of silica dioxide
During the production and use of silica pharmaceutical excipients, many enterprises face serious dust emission issues, leading to raw material waste and workshop environmental pollution. Traditional manual feeding or open conveying methods struggle to meet the cleanliness requirements of Good Manufacturing Practice (GMP), and materials are prone to moisture, clumping, or electrostatic adsorption during transport, affecting subsequent process stability. Additionally, equipment cleaning is cumbersome and maintenance costs are high, which limits improvements in production efficiency.
Material characteristics
Pharmaceutical excipients for silica appear as white powders, with fine particle sizes (usually at the micron level), low density, and average flowability. This material has strong hygroscopic properties and tends to agglomerate in humid environments; At the same time, due to their fine particles, static electricity is easily generated during pneumatic conveying and adsorbed onto the pipe walls. In addition, silicon dioxide is an inert substance, non-toxic and non-corrosive, but it requires high sealing and dust protection in the conveying system to avoid cross-contamination.
Product Introduction

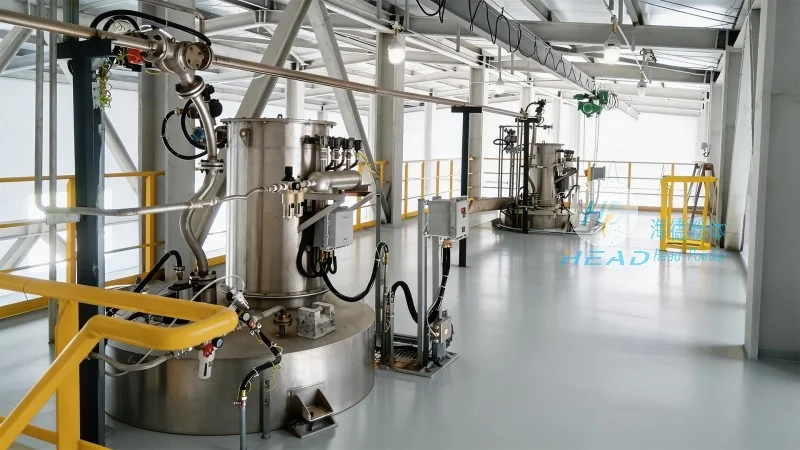
The pneumatic conveying system for pharmaceutical excipients provided by Head Powder is a sealed material transfer solution specifically designed for the pharmaceutical industry. The system uses the principle of pneumatic conveying under positive or negative pressure, accurately transporting silica powder from the storage tank to the production equipment through pipelines. The complete set of equipment includes core components such as feeding devices, gas source processing units, conveying pipelines, gas-solid separators, and automatic control systems, supporting seamless integration with upstream and downstream equipment. Based on customer site layout and capacity requirements, single-point or multi-point conveyor routes can be flexibly customized to achieve fully automated operation.
Product advantages

To address these customer pain points, Head Powder has made targeted optimizations from design to implementation: the system operates in a fully enclosed manner to fully prevent dust leakage and meet GMP cleanliness requirements; Uses anti-static materials and grounding design to effectively eliminate static risks; Equipped with dehumidification and nitrogen protection modules to prevent moisture absorption and deterioration of materials. At the same time, the intelligent control system can monitor conveying pressure, flow rate, and other parameters in real time, supporting remote control and alarm linkage to reduce manual intervention. The modular structure makes assembly and disassembly easy to install, and reduces maintenance costs. With these features, this solution helps customers achieve efficient, stable, and compliant silica pharmaceutical excipient conveying operations.