

Yuxi Yuxi Lithium Battery Graphite Powder Long-distance Pneumatic Conveying with Silo Pump
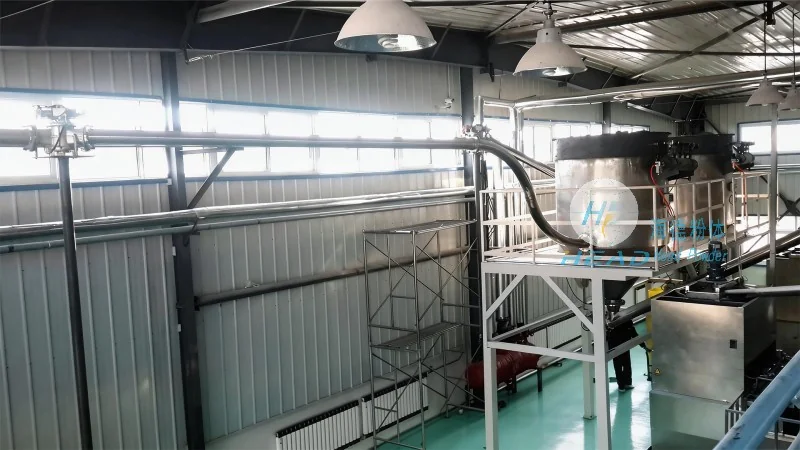
At a lithium battery material production base in Yuxi, Yunnan, we designed and implemented a complete pneumatic conveying system to meet the long-distance transportation needs of graphite powder. This project adopts a long-distance silo pump conveying solution, stably transporting graphite powder from the raw material silo to the batching section, achieving sealed and automated operation throughout the process, which has improved production line efficiency.
Customer pain points

Customers face multiple challenges during production: graphite powder has small particle size and low density, and traditional mechanical conveying easily generates dust and material leakage, leading to harsh workshop environments and high raw material loss; At the same time, when the conveying distance exceeds 300 meters, conventional pneumatic conveying systems often face issues such as pipe blockages, high energy consumption, and low conveying efficiency; In addition, lithium battery graphite powder has strict purity requirements; any external impurities can affect battery performance, thus placing high demands on the sealing and cleanliness of the conveying system.
Solutions and product advantages

To address these pain points, we offer the following targeted solutions:
1. Enclosed long-distance silo pump system: Using the principle of positive pressure concentrated phase conveying, with the silo pump acting as the transmitter, it uses compressed air to deliver graphite powder in a high-concentration, low-speed fluidized manner, effectively reducing the risk of pipeline wear and material crushing. The conveying distance can exceed 500 meters, meeting customers' long-distance needs.
2. Intelligent anti-blocking and pressure stabilization control: Equipped with pressure sensors and PLC automatic adjustment of the air supply valve group, real-time monitoring of pipeline pressure changes, automatically adjusting air volume and blowing frequency to avoid pipe blockages and promote continuous conveying.
3. Fully sealed structure + high-efficiency dust removal: All system interfaces use a double-sealed design, paired with pulse bag dust collectors, keeping workshop dust concentrations below national environmental standards while preventing external impurities from entering, supporting graphite powder purity.
4. Energy-saving and low-consumption operation: By optimizing the gas-solid ratio and pipeline layout, unit energy consumption per unit is reduced by about 30% compared to traditional dilute-phase conveying, saving customers approximately 150,000 yuan in electricity and maintenance costs annually.