

Baking soda pneumatic delivery solution
In many production scenarios, the transportation of baking soda (sodium bicarbonate) faces numerous challenges. Traditional mechanical conveying methods easily cause material blockages, dust accumulation, severe equipment wear, and are difficult to achieve long-distance, enclosed operations. Enterprises often struggle with issues such as low conveying efficiency, high maintenance costs, and environmental pollution, urgently needing a stable, environmentally friendly, and efficient conveyor system to solve these challenges.
Material Characteristic Analysis

Baking soda is a white powder or fine crystals, characterized by easy moisture absorption, clumping easily, average fluidity, and relatively light specific gravity. It has low abrasiveness but tends to adhere to pipe walls in high-humidity environments, requiring high sealing, moisture resistance, and pneumatic parameters of the conveying system. A reasonable pneumatic conveying scheme must fully consider key parameters such as material particle size, humidity, and bulk angle.
Product Introduction
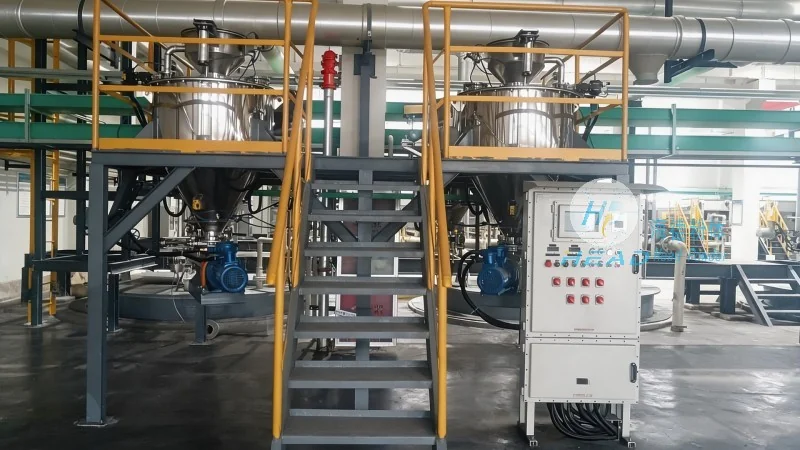
The baking soda pneumatic conveying system provided by Head Powder is a complete set of equipment specially designed for sealed conveying of powder materials. The system is powered by compressed air or inert gases, transporting baking soda from the feeding point to the receiving point through pipelines, covering various forms such as positive pressure conveying, negative pressure conveying, and dense phase conveying. The equipment includes sending tanks, rotary feeders, pipelines, separators, dust collectors, and intelligent control systems. Customized designs can be made according to customer site conditions and process requirements to achieve dust-free, low-energy, and highly reliable material flow.
Product Advantages: Targeted solutions to customer pain points

To address the issue of baking soda easily absorbing moisture and caking, Head Powder System has implemented active moisture-proof measures, including pipeline heating, dehumidification air sources, and material fluidization devices to effectively prevent blockages. To address the challenge of traditional dust conveying, fully enclosed pipelines combined with high-efficiency dust collectors ensure a clean working environment and meet environmental protection standards. To address the pain point of frequent maintenance, the system adopts wear-resistant elbows and quick-open structures to reduce downtime and maintenance time. In addition, the intelligent control system can monitor conveying pressure, material level, and flow in real time, and automatically adjust them via PLC, helping to ensure production continuity.