

Pneumatic conveying solution for cement raw powder
During cement production, the conveying stage of raw powder often faces issues such as dust pollution, pipeline blockages, excessive energy consumption, and limited conveying distance. Traditional mechanical conveying equipment not only has high maintenance costs but also struggles to adapt to complex working conditions, leading to reduced production efficiency and increased environmental pressure. Enterprises urgently need an efficient, sealed, and low-energy delivery solution to address these long-standing pain points.
Material characteristics: Challenges in conveying cement raw powder
Cement raw powder features fine particle size, moisture sensitivity, easy lifting, and large differences in flowability. Their particle size is usually in the tens of microns and contains common moisture, making them prone to adsorption and caking during transportation, causing significant wear on the inner walls of pipelines. Therefore, the conveying system must balance blockage prevention, wear resistance, sealing, and the ability to adapt to changes in material humidity.
Product Introduction: Head Pneumatic Conveying System for Powdered Cement and Raw Powder

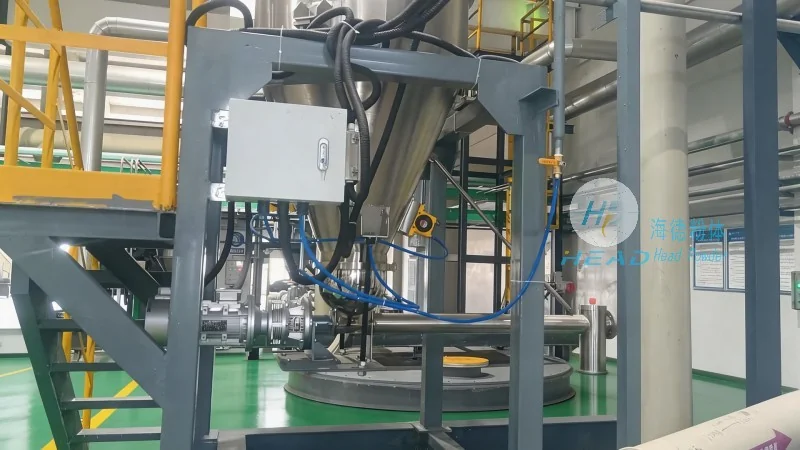
Head Powder is committed to providing customers with customized pneumatic conveying solutions for cement raw powder. This system uses the principle of pneumatic conveying under either positive or negative pressure, delivering raw flour through sealed pipelines through compressed air or vacuum. The system consists of a feeding device, conveying pipelines, air supply equipment, separation and filtration devices, and an intelligent control system. It can be flexibly designed according to the customer's factory layout, conveying distance, and production requirements to achieve fully enclosed, automated, efficient, and stable conveying operations.
Product Advantages: Solutions to pain points

To address the dust, blockage, and high energy consumption issues customers encounter in traditional conveying, Head Powder's solutions offer the following advantages:
- Fully enclosed conveying: Eliminates dust leakage, improves the working environment, and meets environmental protection requirements.
- Strong adaptability: Can handle raw meal powders with different humidity, particle size, and flowability, reducing the risk of pipe blockage.
- Energy saving and consumption reduction: Optimizing air source matching and pipeline design reduces compressed air consumption and lowers operating costs.
- Intelligent control: integrates PLC and monitoring systems to enable remote operation and fault warning, reducing manual intervention.
- Wear-resistant design: Key pipeline parts use wear-resistant materials or linings to extend equipment lifespan.
Head Powder provides full-process services from solution design, equipment manufacturing to installation and commissioning based on customers' actual working conditions, helping the conveying system operate continuously and assisting cement enterprises in improving production efficiency.