

Pneumatic conveying solution for monoammonium phosphate
As a high value-added powder material, monoammonium phosphate is widely used in industries such as fertilizer and chemical engineering. However, during actual production and transportation, enterprises often face issues such as pipeline blockages, low transportation efficiency, and severe equipment wear caused by high moisture absorption of materials. Especially in high-humidity environments, traditional mechanical conveying methods often require frequent shutdowns for cleaning, leading to rising labor costs, production line halts, and overall delivery cycles.
Material characteristics: strong moisture absorption, high adhesion, prone to dust generation

Ammonium phosphate powder has obvious hygroscopic properties; when exposed to air, it easily absorbs moisture, forming clumps or sticking to pipe walls; At the same time, the material particles are fine and dense. If traditional pneumatic conveying systems are not specifically designed, they are prone to uneven conveying, pipeline blockages, dust pollution, and other issues. This requires the conveying solution to balance sealing, anti-sticking and clogging, and low energy consumption.
Product Introduction: Comprehensive solution for monoammonium phosphate pneumatic conveying systems
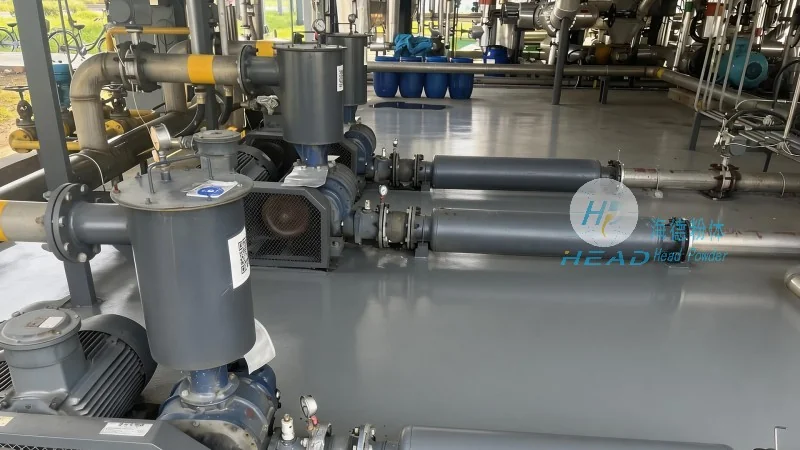
Head Powder offers customized pneumatic conveying system solutions tailored to the physicochemical properties of monoammonium phosphate. This system uses sealed conveying methods of positive or negative pressure, with core equipment including feeders, separators, dust collectors, and intelligent control systems. By optimizing airflow speed, pipe material, and inner wall treatment processes, the adhesion between materials and pipe walls is effectively reduced, while professional dehumidification inlet devices are installed to suppress the risk of caking at the source. The system can flexibly adapt to different production capacity requirements, supporting multi-point feeding and remote monitoring.
Product Advantages: Focuses on pain points, building a stable and efficient conveying closed loop
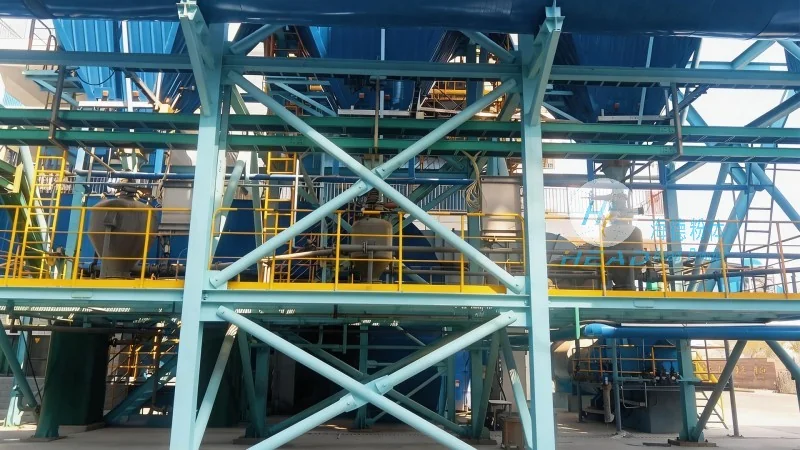
- Anti-blockage design: Uses specially designed smooth lined pipelines and pneumatic artery rush backflow devices to reduce material retention and support continuous operation.
- Humidity control: Integrated air intake drying module lowers the relative humidity inside the system and reduces material moisture absorption.
- Low consumption and energy saving: By dynamically adjusting the gas-solid ratio and conveying pressure, unit energy consumption is reduced and equipment lifespan extended.
- Environmental sealing: Fully enclosed pipeline structure combined with high-efficiency dust collectors curb dust leakage at the source, meeting environmental compliance requirements.