

Pneumatic Conveying Solution for White Sugar Powder
In the processing and packaging stages of white sugar powder, many companies face issues such as dust buildup, moisture accumulation, and equipment blockages during material transportation. Traditional manual handling methods are inefficient and struggle to contribute to cleanliness and hygiene in the production environment. In addition, granulated sugar powder has strong hygroscopic properties and tends to stick easily. Using inappropriate conveying equipment can easily cause material loss and equipment downtime, directly affecting production efficiency and product quality.
Material characteristics

White sugar powder is a fine powdery material, usually with particle sizes ranging from several tens to several hundred microns, and possesses strong hygroscopicity and adhesion. Its fluidity is significantly affected by humidity, making it prone to caking in humid environments and dust to fly around, which places high demands on the sealing and moisture-proof performance of the conveying system. At the same time, granulated sugar powder is a food raw material, so the transportation process must comply with relevant hygiene standards to avoid secondary contamination.
Product Introduction
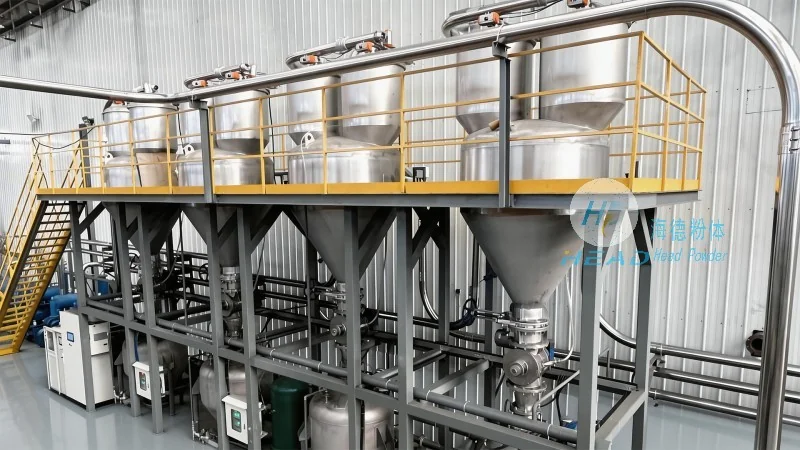
The pneumatic conveying system provided by Head Powder uses sealed pipelines for positive or negative pressure conveying, enabling automated transfer of sugar powder from raw material warehouses to production equipment or packaging stations. The system includes air supply devices, feeders, conveying pipelines, dust separation equipment, and control systems, and can be customized according to user workshop layout, conveying distance, and production capacity requirements. The entire machine is made of stainless steel, with a smooth interior without dead corners, making cleaning and maintenance easy, effectively preventing material residue and cross-contamination.
Product advantages
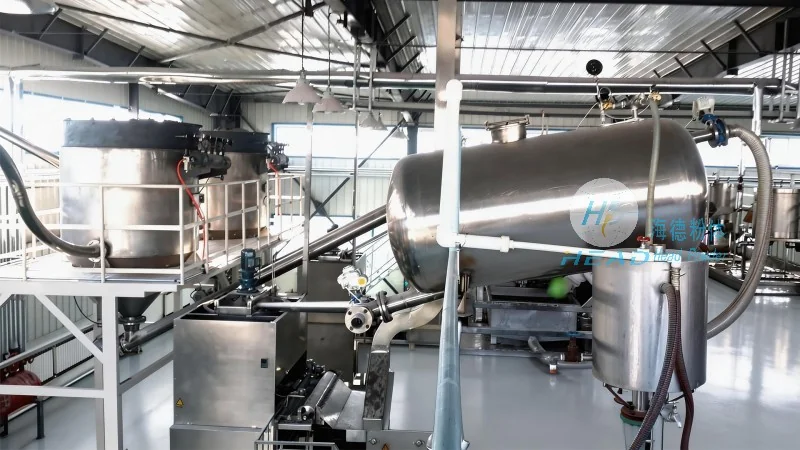
To address customer pain points, Head Powder focuses on solving the following issues in its pneumatic conveying solution for white sugar powder: First, it adopts a fully enclosed conveying path to fully prevent dust leakage and improve the workshop environment; Second, it is equipped with moisture-proof and dehumidifying devices and pipeline heat tracing options to reduce the risk of material moisture absorption and caking; Third, wear-resistant and non-stick coatings are applied at the feeder and elbows to reduce clogging and wear; Fourth, an integrated intelligent control system can monitor conveying pressure, flow, and material level in real time, enabling fault early warning and remote operation, improving operation and maintenance convenience. The entire system supports hygiene and safety while improving conveying efficiency and reducing labor and maintenance costs.