

Pneumatic conveying solution for protein powder
In the production and processing of protein powder, traditional manual or mechanical conveying methods often face many challenges: powders easily absorb moisture and clump together, causing blockages in pipelines or equipment; Severe dust swirling not only pollutes the production environment but may also cause safety hazards from dust explosions; At the same time, manual operation efficiency is low, making it difficult to meet the demands of continuous and large-scale production. Moreover, as a high value-added product, protein powder requires high cleanliness, hygiene, and cross-contamination prevention. How to achieve sealed, efficient, and low-loss conveying has become a major challenge for the industry.
Material properties: the physical and chemical characteristics of protein powder

Protein powder is a lightweight, fine-grained material, usually ranging from several tens to hundreds of microns, with low density and average flowability. It is highly hygroscopic, easily clumps in humid environments, and is sensitive to temperature, possibly deforming at high temperatures. At the same time, protein powder tends to generate static electricity during conveying, posing a common dust explosion risk (such as corn protein powder, soy protein powder, etc.). Therefore, the conveyor system must be airtight, moisture-proof, anti-static, explosion-proof, and easy to clean.
Product Introduction: Pneumatic protein powder conveying system equipment

Head Powder provides customized pneumatic conveying solutions tailored to the material characteristics of protein powder and industry pain points. The system uses positive or negative pressure conveying methods, delivering protein powder from the feeding end to the process (such as mixing, packaging, storage, etc.) more accurately through sealed pipelines. The equipment includes air supply systems (blowers or vacuum pumps), feeders (such as rotary valves, Venturi injectors), conveying pipelines, separation devices (such as cyclone separators, baghouse dust collectors), and automated control systems. All contact materials are made of food-grade stainless steel, with polished surfaces and no blind spots, meeting hygiene standards. The system can be flexibly configured according to production capacity (e.g., 1-10 tons/hour), conveying distance (10-100 meters), and site conditions.
Product Advantages: Targeted solutions to customer pain points
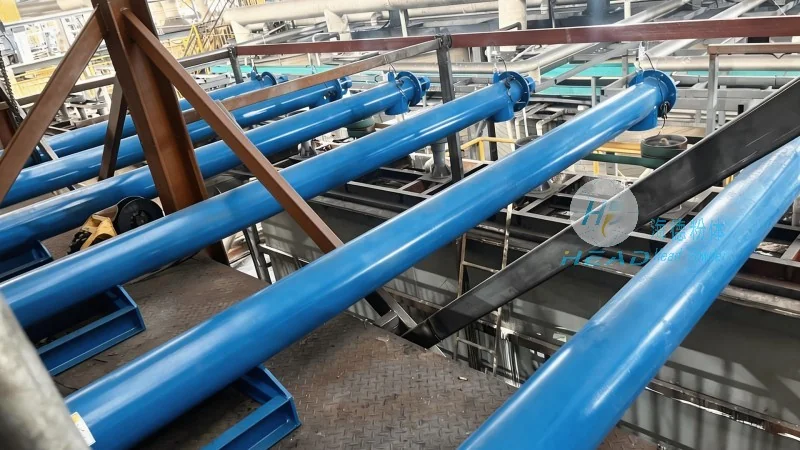
Head Powder's protein powder pneumatic conveying system has the following main features:
- Sealed conveying to prevent dust leakage:The entire pipeline is sealed and operated with no leakage, preventing protein powder moisture absorption and workshop pollution, while also reducing the risk of dust explosions.
- Moisture-proof and anti-caking design:The system is equipped with dehumidification devices or heat tracing temperature control functions to preprocess the transported gases and prevent materials from becoming damp and sticking inside the pipeline.
- Intelligent control to improve efficiency:Equipped with PLC + touchscreen automatic control system, it can monitor parameters such as conveying pressure, flow, and material level in real time, achieving relatively accurate feeding and continuous normal operation, reducing manual intervention.
- Safety Protection System:Equipped with anti-static grounding, explosion relief devices, inert gas protection, or oxygen content monitoring, the system helps operate within safe production limits.
- Easy to maintain and clean:Quick-release structural design facilitates cleaning of pipelines and equipment interiors, meeting hygiene requirements when switching between multiple product types.
Through these designs, Head Powder helps customers achieve automation, safety, and cleanliness in protein powder conveying processes, reducing operating costs and improving product quality stability.