

Pneumatic conveying solution for soy protein powder
During the production and processing of soy protein powder, enterprises often face issues such as low material conveying efficiency, severe dust pollution, and high equipment maintenance costs. Traditional mechanical conveying methods easily cause material damage, difficult residue removal, and cannot meet the demands of sealed and automated production. In addition, soy protein powder is prone to moisture absorption and clumping, making it difficult for conventional conveying systems to support its flow and stability, directly affecting production rhythm and finished product quality.
Material characteristics: Difficulties in conveying soy protein powder
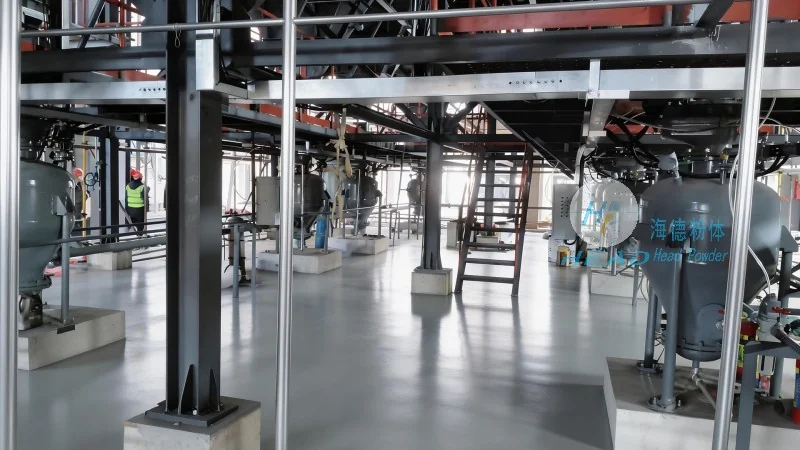
Soy protein powder is a lightweight, fine-grained material, usually between 80~200 mesh and a bulk density of about 0.4~0.6 g/cm³. It features low flowability, easy lifting, and strong moisture absorption. During transportation, materials tend to adhere and agglomerate on the inner walls of pipelines, and may even become blocked. At the same time, their fine particles easily generate static electricity, increasing the risk of explosion, so high requirements are placed on the airtightness, explosion-proof performance, and cleaning capacity of the conveying system.
Product Introduction: Pneumatic conveying system for soy protein powder
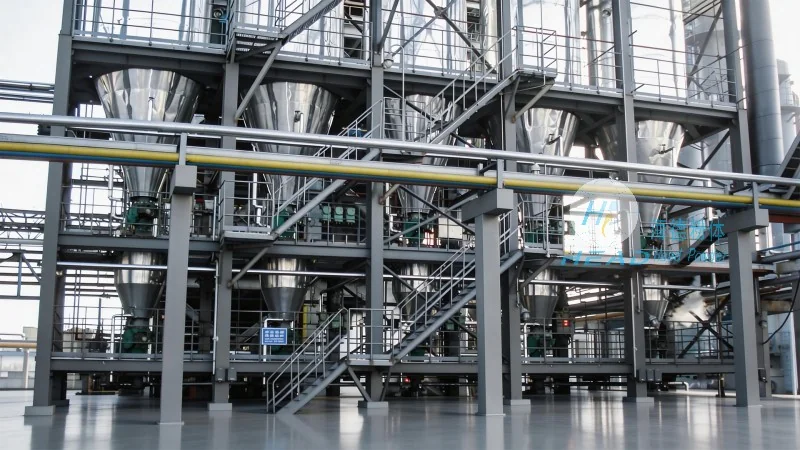
The pneumatic conveying system for soybean protein powder provided by Head Powder uses sealed pipeline conveying methods of positive or negative pressure, utilizing compressed air as the power source to achieve automated transfer of materials from raw material warehouses to downstream production equipment. The system consists of a feeding device, conveying pipelines, air source equipment, dust separation and removal unit, and an intelligent control system, allowing for customized design based on customer capacity, workshop layout, and process requirements. The equipment is made of stainless steel, with smooth inner walls without dead corners, meeting food-grade hygiene standards. It is also equipped with explosion-proof pressure relief devices and pulse reverse blow filtration systems, ensuring safe operation and meeting environmental protection standards.
Product Advantages: Targeted solutions

To address these customer pain points and material characteristics, Head Powder has made special optimizations from system design and core components to control strategies: adopting low-speed dense phase conveying technology to reduce material crushing and pipeline wear; Equipped with online dehumidification and anti-arching devices to ensure smooth material flow; Sealed pipelines and negative pressure environments effectively suppress dust leakage, improving the workshop working environment; The intelligent control system can monitor material flow, pressure, and air volume in real time, enabling more accurate feeding and fault alarms, thereby reducing manual intervention and operation and maintenance costs. The complete solution helps enterprises improve production efficiency, reduce material waste, and meet food safety and environmental compliance requirements.