

Pneumatic Xylitol powder conveying solution
In the food, pharmaceutical, and chemical industries, the transportation of xylitol powder often faces challenges such as dust swirls, material clumping, pipeline blockages, and cross-contamination. Traditional mechanical conveying methods are not only inefficient but also struggle to support product purity and the cleanliness of the production environment. To address these practical challenges, Head Powder, leveraging years of experience in pneumatic conveying, has launched customized xylitol powder pneumatic conveying system equipment, helping enterprises achieve efficient, sealed, and stable material flow.
Material characteristics

Xylitol powder features strong hygroscopicity, relatively fine particle size (usually 100-400 mesh), moderate fluidity, easy static electricity, and sensitivity to temperature. During conveying, if the ambient humidity is too high or the system design is improper, powder may stick together or clump together, affecting subsequent processes. Additionally, as a food additive, xylitol requires strict hygiene standards for conveying equipment, avoiding the contamination of metal foreign matter and microbial growth.
Product Introduction

The xylitol powder pneumatic conveying system provided by Head Powder uses positive pressure dilute phase or dense phase conveying methods. The entire equipment consists of a gas source, feeding device, conveying pipelines, dust separation and removal, and an intelligent control system. The system can be customized according to material characteristics and on-site conditions, such as using stainless steel, adding dehumidification and cooling modules, and equipping anti-static measures, helping xylitol maintain stable physical and chemical properties throughout the entire transport process. At the same time, the system uses fully sealed circulation pipelines to prevent dust leakage and meets GMP clean production requirements.
Product advantages
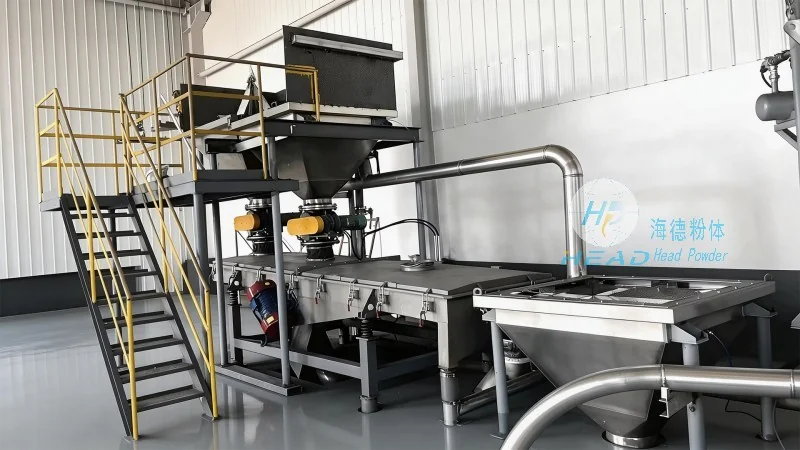
To address common customer concerns such as dust leakage, blockages, shutdowns, and high energy consumption, Head Powder has focused on strengthening the following aspects in its xylitol pneumatic conveying solution: First, by optimizing airflow control and pipeline layout, the probability of material deposition at elbows and valves is effectively reduced; Second, it introduces online cleaning and moisture removal interfaces to facilitate regular system cleaning and reduce the risk of microbial growth; Third, it uses a modular control unit that can monitor conveying pressure, flow, and material level in real time, automatically adjusting air supply volume, balancing delivery efficiency and energy consumption. The entire system is food-grade validated, helping customers improve production line continuity and reduce labor maintenance costs.