

Complete Rare Earth Powder Inert Gas Transportation Project in Baoji, Shaanxi

This project is located in Baoji, Shaanxi. A certain enterprise needs to transport rare earth powders over long distances in a sealed manner. Rare earth powders are characterized by high value, easy oxidation, fine particles, and easy flight. During transportation, it is recommended to isolate them from air to avoid contact with moisture or oxygen, which can lead to quality degradation. The customer's original manual handling method was inefficient, caused severe dust pollution, and could not meet the requirements for inert gas protection.
Customer pain points
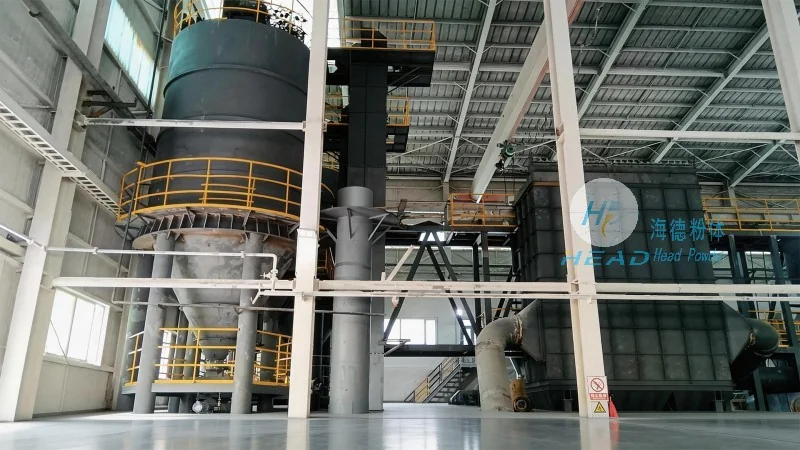
1. Powder oxidation issues: Rare earth powders are highly prone to oxidation and discoloration when exposed to air, affecting product purity and final performance. 2. Environmental pollution and loss: Traditional manual feeding and transportation processes generate large amounts of dust, which not only waste materials but also pose threats to the workshop environment and operator health. 3. Low conveying efficiency: Multi-stage handling and intermittent operations take a long time to keep pace with the continuous production rhythm of subsequent processes. 4. Safety and Sealing Requirements: The conveying system must be filled with inert gases (such as nitrogen) throughout the process, but conventional equipment struggles to achieve high sealing and gas recovery. 5. Complex equipment maintenance: Powder easily sticks to and becomes blocked on the inner walls of pipelines, and frequent cleaning disrupts production schedules.
Product advantages
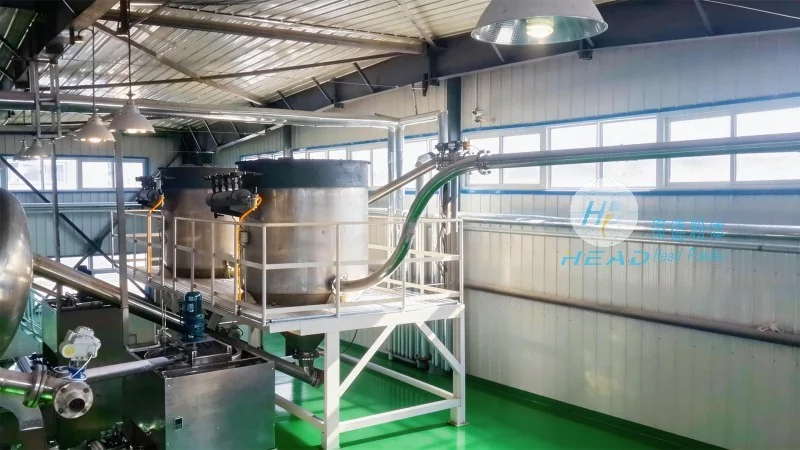
To address these pain points, Head Powder offers customized pneumatic conveying system solutions:
Sealed inert gas protection: The system adopts a fully enclosed pipeline design, combined with nitrogen circulation and pressure balancing devices, keeping the rare earth powder in an inert atmosphere throughout, effectively preventing oxidation and reducing nitrogen consumption.
Low wear and residue: Selected polished stainless steel pipes and elbows on the inner wall, combined with an appropriate gas-solid ratio and flow rate, reduce powder impact and friction on the pipe wall, with residual rate in the pipeline below 0.5% after transportation.
Intelligent control and online monitoring: Integrated PLC and touchscreen, real-time display of material-air ratio, pressure, oxygen content, and other parameters, automatically adjusting air replenishment volume and conveying speed, with abnormal alarm and emergency shut-off functions to help ensure stable normal operation.
Modular design supports maintenance: Each section of the system uses flange connections and quick-open structures, allowing quick removal and blockage removal during maintenance; Key wear parts (such as sealing rings and valves) use standard parts, making replacement easy and reducing downtime.
Environmental protection and energy saving: Equipped at the end with high-efficiency baghouse dust collectors and return air pipelines, dust emission concentration below 5mg/m³, while partially recovering nitrogen for recycling, reducing overall energy consumption by about 30% compared to traditional methods. This solution has been successfully applied to a rare earth processing production line in Baoji. After commissioning, material loss was reduced by 92%, conveying efficiency tripled, and the workshop environment met cleanliness standards.