

Case Study of Sealed Conveying of Ultrafine Powder in Xiaogan, Hubei Fine Chemical
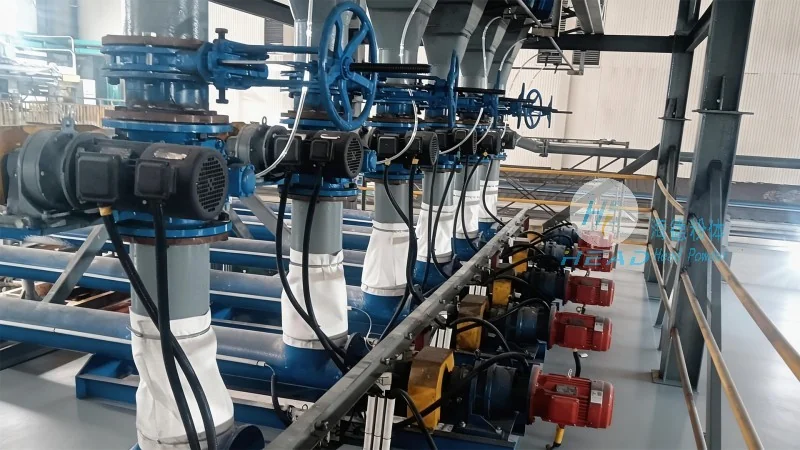
A fine chemical company located in Xiaogan, Hubei, has long been engaged in the research, development, and production of ultrafine powders. Due to the extremely small powder particle size, which easily generates dust and absorbs moisture, the original open-mouth conveying method led to severe dust pollution in the workshop, high material loss, frequent equipment maintenance, and pose health risks to personnel. Enterprises urgently need a safe, environmentally friendly, and efficient sealed conveying system to improve both the production environment and product quality.
Customer pain points

The core pain points faced by the company include: (1) Ultrafine powder easily generates dust during transportation, and traditional mechanical conveying equipment lacks sealing, leading to excessive PM2.5 in workshops and significant environmental pressure; (2) Powder absorbs moisture and causes caking, causing pipeline blockages and equipment downtime, affecting continuous production; (3) Material loss rate as high as 3%-5%, with significant economic costs; (4) Heavy manual cleaning and equipment maintenance workload, with low operational efficiency; (5) Existing equipment cannot meet increasingly stringent industry environmental and safety standards.
Product advantages
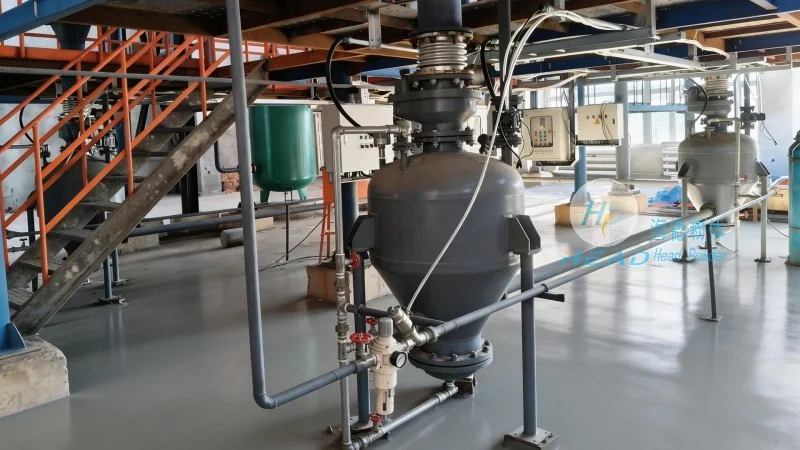
Head Powder addresses these pain points by providing a comprehensive solution based on sealed pneumatic conveying technology. This system adopts a fully enclosed pipeline design, allowing materials to be transported under the action of negative or positive pressure airflow, with no dust leakage throughout the process, thereby improving dust issues. To address the moisture-prone nature of ultrafine powders, the system is equipped with nitrogen protection and drying pretreatment modules to prevent caking and blockage. At the same time, through more accurate airflow control and intelligent monitoring systems, material loss is kept below 0.5%, reducing operating costs. The equipment operates stably and is easy to maintain, helping customers achieve clean production and ongoing compliance.