

Pneumatic cocoa powder conveying solution
In the processing and production of cocoa powder, the conveying stage is often the key factor affecting overall efficiency and product quality. Traditional methods often face issues such as dust pollution, material clumping, and low conveying efficiency, which severely restrict the normal operation of production lines. To this end, we offer pneumatic conveying solutions specifically designed for the characteristics of cocoa powder, helping customers achieve efficient, clean, and safe material flow.
Customer pain points
Many cocoa powder manufacturers report frequently encountering the following problems during transportation: materials easily absorb moisture and clump together, leading to pipeline blockages; Severe dust swirling not only pollutes the workshop environment but also poses explosion risks; Limited conveying distance, making flexible layout difficult; Frequent equipment maintenance increases operating costs. These issues directly affect product quality and production continuity.
Material characteristics
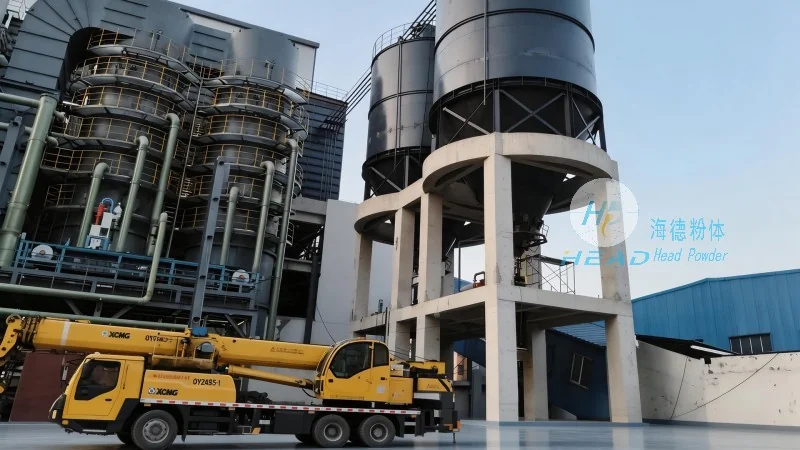
Cocoa powder, as a fine powdered material, features small particle size, low density, easy moisture absorption, high oil content, and easy adhesion. During conveying, it has a high friction coefficient on the pipe wall and is sensitive to temperature and humidity, making it prone to accumulation and deterioration in dead corners. Therefore, it is recommended that the conveying system have good sealing, moisture resistance, and appropriate flow rate control to help maintain the original quality of the material during transfer.
Product Introduction
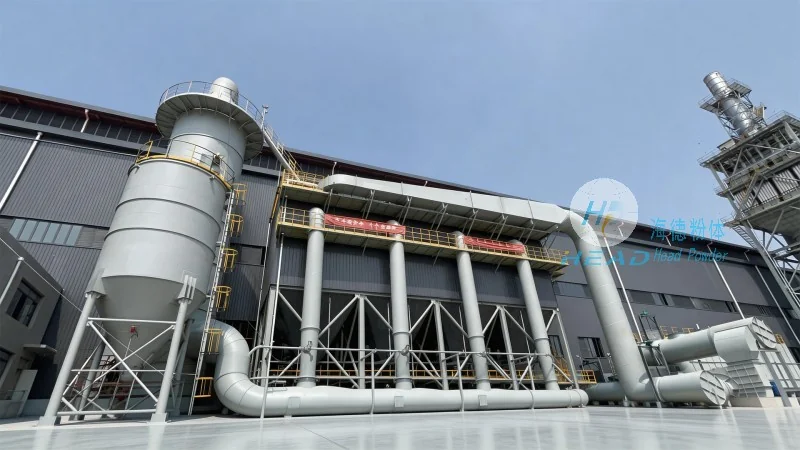
The cocoa powder pneumatic conveying system provided by Head Powder uses either positive or negative pressure conveying methods, allowing for customized design according to customer site conditions and conveying requirements. The core components of the system include the feeding device, delivery pipeline, air supply equipment, and separation and filtration device, all made from wear-resistant and easy-to-clean materials. To address the adhesion characteristics of cocoa powder, the inner walls of pipes are specially treated, and pneumatic blocking accessories are installed to effectively reduce residue and blockage. The entire system enables efficient and sealed conveying from the storage silo to the packaging line or other workstations, with no dust leakage throughout the process.
Product advantages

To address customers' pain points in conveying efficiency, environmental protection, and maintenance, our solutions feature the following application features:
- Sealed transport to eliminate dust: Fully enclosed duct design controls dust dispersion from the source, significantly improving workshop air quality while reducing explosion risk, meeting strict environmental and safety standards.
- Anti-caking design ensures stability and reliability: By optimizing airflow speed and pipeline paths, combined with the automatic-surge backblow system, it effectively prevents cocoa powder from sticking or clumping inside the pipeline, facilitating long-term continuous operation.
- Intelligent control reduces manual labor: Integrated PLC control system can monitor conveying pressure, flow, and material level in real time, automatically adjust operating parameters, reduce manual intervention, and lower the probability of operational errors.
- Customized solutions, flexible matching: Based on customers' different production capacities, workshop layouts, and material characteristics, we offer customized solutions for conveying from single points to multiple points, horizontal or vertical conveying, largely adapting to existing production processes.