

Pneumatic conveying solution for phosphate ore powder
In industrial scenarios such as phosphate chemical and fertilizer production, the transportation of phosphate ore powder has long faced practical issues such as dust pollution, severe equipment wear, high energy consumption, and limited conveying distances. Traditional mechanical conveying methods (such as screw and belt conveying) easily cause material leaks, excessive environmental dust levels, frequent equipment maintenance, and high operating costs. How to achieve sealed, efficient, and low-consumption phosphate powder transportation has become an urgent pain point for many enterprises to solve.
Material Property Analysis: Physical parameters of phosphate ore powder
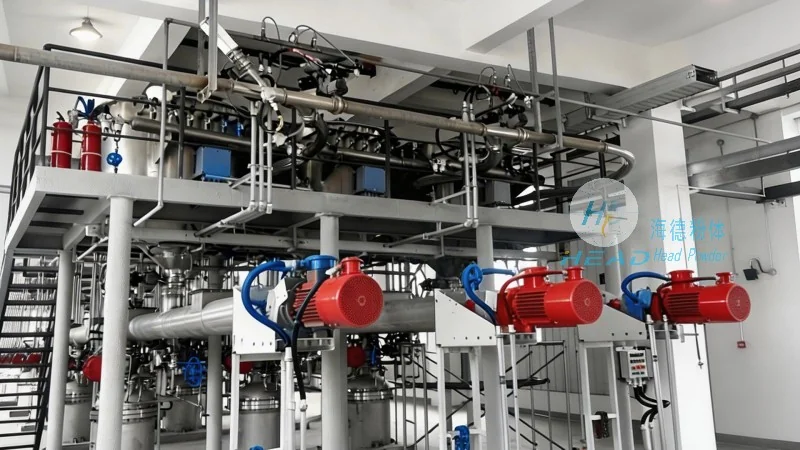
Phosphate ore powder is generally fine powder, with a density of about 1.2~1.6 t/m³, particle sizes mostly distributed between 0.1~0.5 mm, and usually low moisture content, exhibiting typical abrasiveness and corrosiveness. These materials have average flowability and are prone to static electricity and agglomeration during transportation, placing high demands on the sealing, wear resistance, and anti-clogging capabilities of the conveying equipment.
Product Introduction: Pneumatic conveying system for phosphate ore powder

The phosphate powder pneumatic conveying solution provided by Head Powder is a complete conveying system designed specifically for the unique properties of phosphate powder. This system uses compressed air or fans as power sources and achieves fixed-point delivery of phosphate powder through sealed pipelines, effectively preventing dust leakage while reducing equipment wear and maintenance frequency. The system can be customized non-standard according to user site space, conveying distance, and conveying volume, suitable for various pneumatic conveying forms such as positive pressure dense phase, dilute phase, or negative pressure, meeting different working conditions.
Product Advantages: Targeted solutions to customer pain points
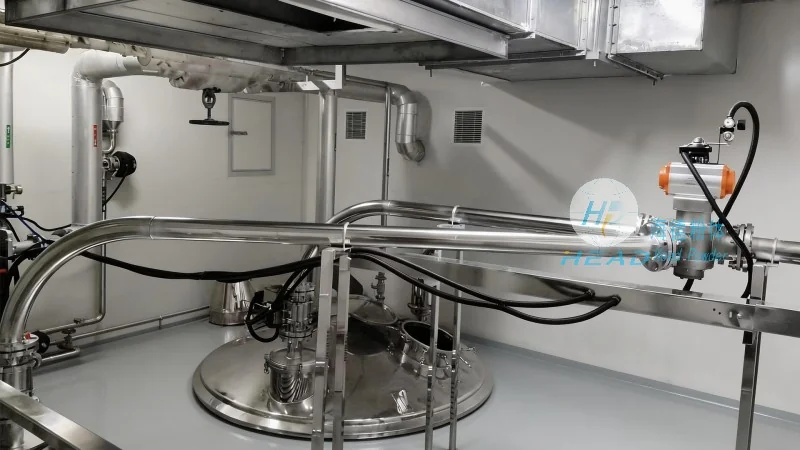
To address core pain points customers encounter in phosphate powder transportation—such as environmental protection, energy consumption, and maintenance—the Head Powder Pneumatic Conveying System offers the following solutions:
- Fully sealed conveying: The pipeline system has no leakage points, effectively controls dust dispersion, improves the workshop environment, and meets environmental protection requirements.
- Low energy consumption design: Optimized gas-solid ratio and pipeline layout reduce unit energy consumption compared to traditional methods, resulting in better long-term operating costs.
- High wear-resistant configuration: Key components (such as elbows, valves, pipeline linings) are made of wear-resistant materials to extend equipment service life and reduce downtime for maintenance.
- Intelligent control: Equipped with a PLC automatic control system, it can monitor conveying pressure, flow, material level, and other parameters in real time, enabling unmanned operation and fault warning.