

Lactose pneumatic conveying solution
During lactose processing and production, enterprises often face challenges such as material moisture absorption and clumping, high particle crushing rates, and dust leakage polluting the environment. Traditional mechanical conveying methods not only have low efficiency but also easily cause product loss and difficulties in equipment cleaning, affecting final product quality and production efficiency.
Material characteristics: A key consideration for lactose conveying
Lactose is a white crystalline powder with normal hygroscopic properties. The granules are relatively brittle, have average flowability, and are sensitive to temperature changes. These characteristics require strict control of environmental humidity, conveying speed, and the material of contact components during conveying to maintain the original shape and purity of the material.
Product Introduction: Lactose pneumatic conveying system

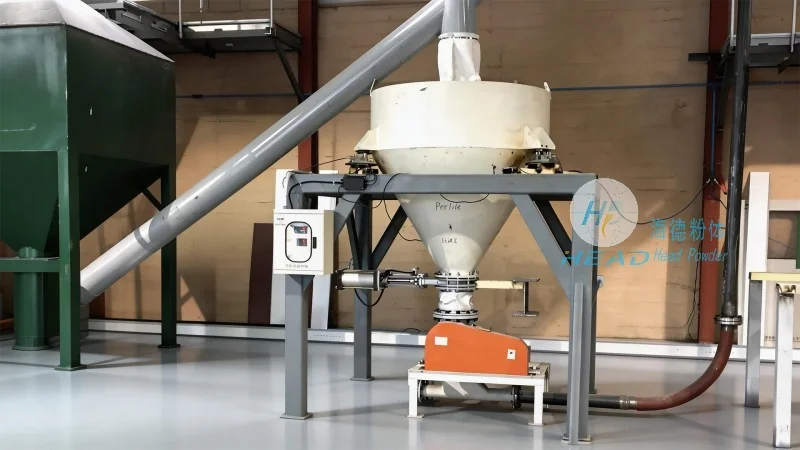
Head Powder offers customized pneumatic conveying solutions tailored to the characteristics of lactose materials. The system adopts a fully enclosed pipeline design, using airflow as the power carrier, and achieves safe and clean delivery of lactate through positive or negative pressure. Depending on production site conditions, conveying distance, and capacity requirements, the conveying modes can be flexibly configured to meet the application requirements of enterprises of different sizes.
Product Advantages: Targeted solutions to customer pain points

1.Dust-free, sealed, and conveyed without dust: The system operates in a sealed seal throughout, effectively preventing lactose moisture absorption, dust, and external pollution, improving the workshop environment. 2.Low damage protection: By optimizing airflow velocity and pipe structure, collisions and friction between particles are reduced, lowering the lactose breakdown rate. 3.Flexible customization: Based on output, material characteristics, and site layout, we offer personalized solution designs to help improve conveying efficiency and stability. 4.Easy to maintain and clean: The system structure is simple, supports quick disassembly and cleaning, meeting hygiene requirements in the food and pharmaceutical industries. 5.Intelligent control: Equipped with an automated control system to monitor conveying status in real time, reduce manual operation errors, and improve overall operational reliability.